SLAG & DROSS REMOVAL · BB CONFIGURATION
BB Belt Slag Removal Machine
Two abrasive belt stations remove standard dross, slag beads and oxide skin from thermal-cut carbon steel parts, then level the surface for welding, coating or assembly — without manual chipping and grinding between operations.
- Two-belt configuration
- 800–1,600 mm working widths
- For plasma-, flame- and laser-cut carbon steel
- Standard dross removal in a single pass
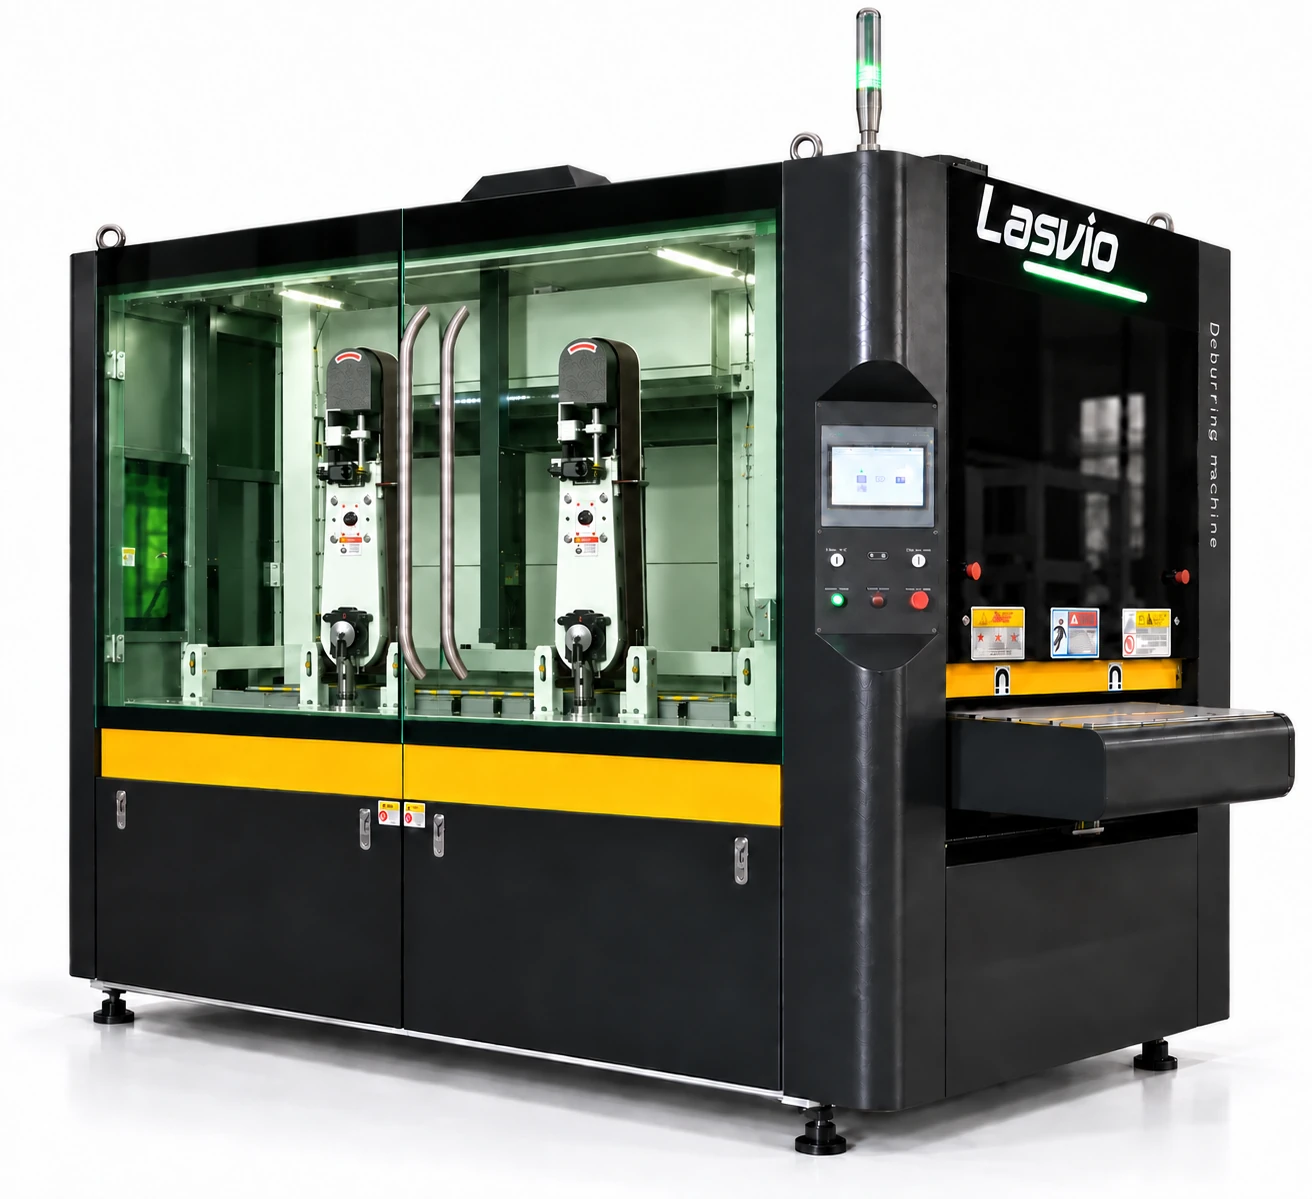
Configuration: 2 abrasive belt stations
Working Width: 800 / 1,000 / 1,300 / 1,600 mm
Processing Thickness: 0.5–80 mm
Hold-Down: Magnetic table for carbon steel
Built for Standard Dross — Not Heavy, Hammer-Hard Slag
Plasma cutting, flame cutting and other thermal cutting processes can leave resolidified material attached around cut edges and holes. The BB is designed for the deposits an abrasive belt can break loose and strip directly: everyday dross and moderate slag that would otherwise be removed by hand, one part at a time.
If the deposit is thick, strongly bonded and cannot be broken by a belt alone, it is no longer a BB job. The slag should be fractured first with a hammer station — see the HB and HBB configurations below.
What BB is made to remove
- Dross beads around cut edges and holes
- Light-to-moderate slag from plasma and flame cutting
- Oxide skin left around the cut profile
- Surface contamination that slows welding and coating preparation
- The manual chipping and grinding bottleneck after thermal cutting
Inside the BB: Two Belts, Two Jobs
The BB uses two belt stations in sequence. The first station does the breaking and stripping; the second removes what is left and levels the surface. Separating the two jobs lets each belt work with the grit and settings suited to its stage of the process.
Part flow runs from the entry-side belt station to the exit-side finishing belt.
Station 1 — Coarse Abrasive Belt
The entry-side belt makes first contact with the part. Its coarse abrasive breaks loose and strips dross, slag beads and oxide skin from the surface and around the cut profile.
Station 2 — Finer Abrasive Belt
The exit-side belt removes the remaining deposits and levels the surface, leaving the part clean and consistent for the next operation.
Magnetic hold-down: carbon-steel parts are held flat on the magnetic conveyor without clamps, so small parts can run safely at production feed speed.
Processing Capability
The BB is a through-feed deslagging machine for thermal-cut carbon steel. In one pass it removes the slag and dross left by plasma cutting, flame cutting and laser cutting, pre-grinds the surface, and leaves every part clean and consistent for the next process.
- Slag & dross removal — Strips resolidified slag and dross from plasma- and flame-cut carbon steel parts.
- Oxide skin removal — Removes the oxide layer left around thermal-cut profiles before further processing.
- Surface pre-grinding — The second belt pre-grinds and levels the surface in the same pass.
- Holes & edges cleaned — Clears dross build-up around holes and cut edges, where manual cleanup is slowest.
- Uniform one-pass result — Every part receives the same two-belt treatment, with no operator-dependent variation from manual grinding.
- Ready for the next process — A clean, consistent surface that forms a solid foundation for welding, coating and assembly.
Cleaner Parts in One Pass
No Separate Chipping Step
Standard dross is removed inside the through-feed process instead of at a separate manual workstation.
Ready for Welding or Coating
Removing dross, slag beads and oxide skin prepares cleaner edges and surfaces for the next fabrication process.
Repeatable From Part to Part
A fixed two-belt process gives a more consistent result than manual grinding that depends on the operator and the time available.
Before and After One BB Pass
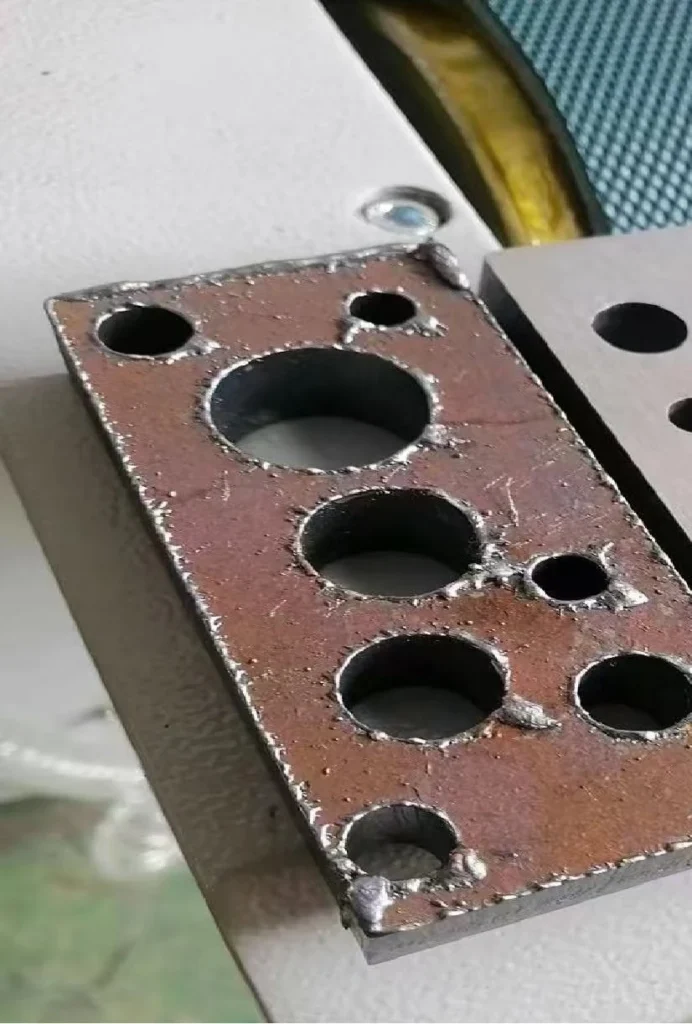
BEFORE
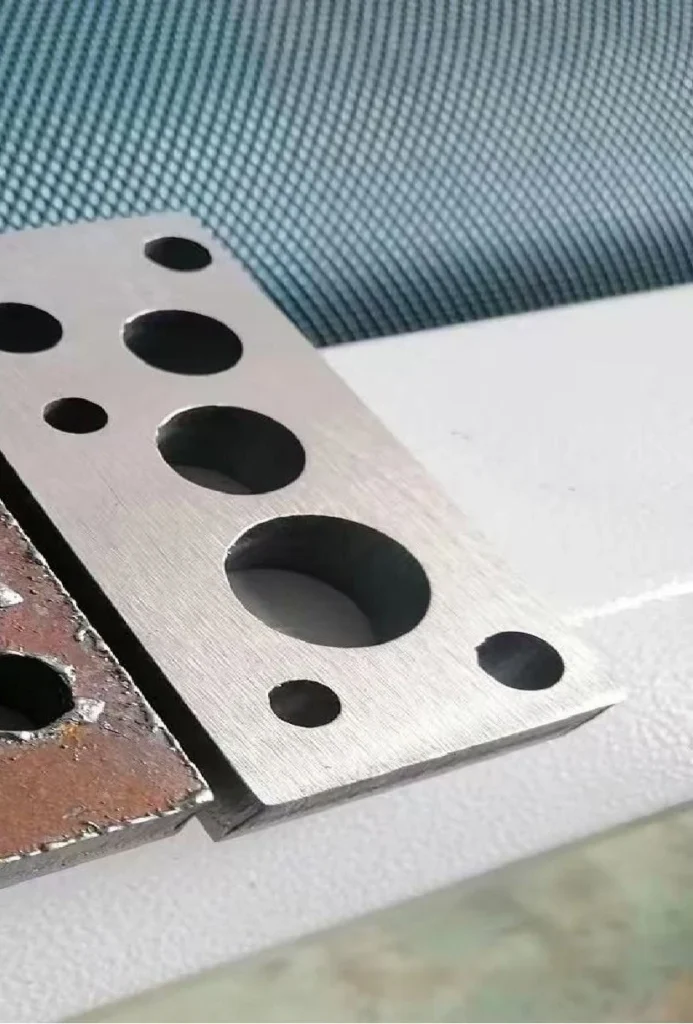
AFTER — ONE PASS
A plasma-cut carbon-steel plate after one BB pass — dross gone, holes and edges clean, and the surface ready for coating or welding.
BB Is the Right Choice When…
- Your parts are carbon steel.
- The main problem is standard dross or moderate slag.
- Parts come from plasma, flame or laser cutting.
- You do not need a dedicated edge-rounding station.
- You want to replace manual chipping and grinding with a repeatable process.
Choose Another Configuration When…
- Heavy, hard slag: choose HB — the hammer station fractures the slag before belt finishing.
- The heaviest slag and a cleaner finish: choose HBB — hammer impact followed by two abrasive belts.
- Deburring plus controlled edge rounding: move to the BR / HBR / BBR / BRB configurations in Deburring & Edge Rounding.
BB vs. HB vs. HBB
| BB | HB | HBB | |
|---|---|---|---|
| Station sequence | Belt + Belt | Hammer + Belt | Hammer + Belt + Belt |
| Best for | Standard dross and moderate slag | Heavy, hard slag | The heaviest slag, with a cleaner finished surface |
| Choose it when | A belt can break and strip the deposit directly | The deposit must be fractured before belt finishing | Slag-breaking power and surface finish are both critical |
BB Technical Specifications
| Configuration | BB — two abrasive belt stations |
| Working Widths | 800 / 1,000 / 1,300 / 1,600 mm |
| Main Process | Standard dross removal, slag removal and abrasive surface levelling |
| Typical Parts | Plasma-cut, flame-cut and laser-cut carbon steel parts |
| Processing Thickness | 0.5–80 mm |
| Feeding Speed | 1–5 m/min |
| Sanding Belt Speed | 5–13 m/min |
| Hold-Down | Magnetic conveyor table |
| Power Supply | 380 V AC, 50/60 Hz (customizable) |
| Air Pressure Required | 0.5–0.8 MPa |
| Service | CE Certified · Global Service |
All listed safety, servo-control, electrical and auto-compensation features are standard equipment.
BB Slag Removal Machine — Frequently Asked Questions
What does the Lasvio BB remove?
The BB removes standard dross, slag beads and oxide skin from thermal-cut carbon steel parts, including deposits left around cut edges and holes by plasma and flame cutting.
Can the BB remove heavy slag?
BB is not the heavy-slag configuration. If the slag is thick and strongly bonded, choose HB or HBB so a hammer station can fracture it before the abrasive belt finishes the surface.
Does the BB round edges?
No. BB is a two-belt slag and dross removal configuration and does not include a dedicated rotary-brush edge-rounding station. For deburring with controlled edge rounding, see the BR, HBR, BBR and BRB configurations.
Which materials is BB designed for?
BB is designed around carbon-steel parts because it uses a magnetic hold-down table. If your parts are non-magnetic or also need edge rounding or a controlled surface finish, send us the part details so we can recommend the right configuration.
How do I confirm whether BB fits my parts?
Send the material, thickness, part size, cutting process and clear photos of the slag on both sides — or arrange a sample test on your actual parts. That is the most reliable way to confirm the configuration and belt setup.
Send Your Parts for a BB Test
Tell us what you cut, how the slag looks, and what happens to the part next. We will confirm whether BB is sufficient — or whether your parts need the hammer station in HB or HBB.
Request a Quote Chat on WhatsApp
Compare all slag removal configurations Installation, warranty and support
← Back to Slag & Dross Removal Next: HB Heavy Slag Removal →