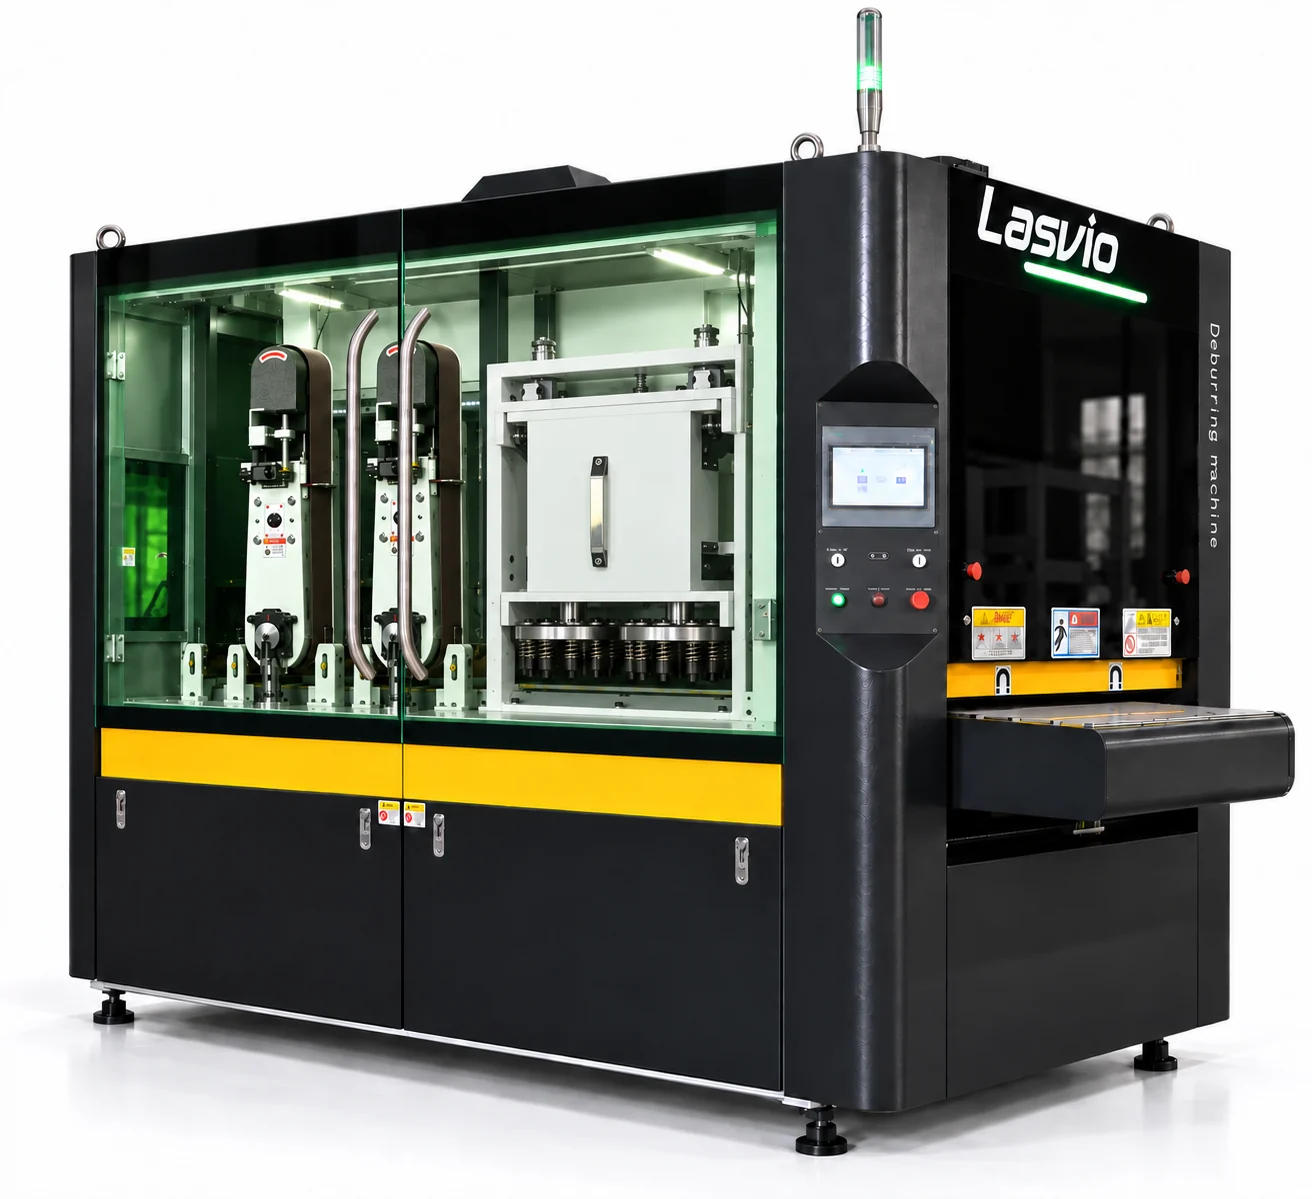
HEAVY SLAG REMOVAL MACHINE

Heavy Slag Removal Machines for Thermal Cut Steel Parts

Remove stubborn slag and dross from plasma-cut, oxy-fuel-cut, and thick thermal-cut steel parts before welding, coating, or edge rounding.

800mm-1600mm31.5-63.0 inches working width
Thermal Cut PartsPlasma, oxy-fuel and thick steel parts
CE CertifiedBuilt to international safety standards
Global ServiceRemote support and overseas service available

Common Processing Challenges

Heavy slag after thermal cutting creates multiple production problems.
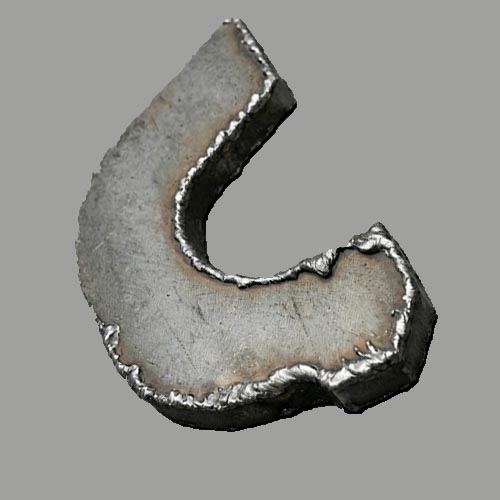
Plasma cutting, oxy-fuel cutting, and thick-plate thermal cutting can leave hard slag attached to the bottom edge of the part. If it is removed manually, the process becomes slow, inconsistent, and dependent on operator skill.

Time-consuming manual grinding

Poor welding preparation

Inconsistent slag removal quality

Increased labor cost

Secondary processing delays

Powder coating adhesion issues

For fabrication shops processing thermal-cut steel parts, slag removal is often the first bottleneck before welding, coating, and assembly. A dedicated slag removal machine helps reduce manual grinding and makes the downstream process more repeatable.

What Is It Built For?

Built for standard dross and heavy thermal-cut slag.
Choose BB for standard dross and general burr removal. HB and HBB use hammer-disc impact to fracture heavy slag before abrasive-belt finishing.
Typical Applications
Plasma-cut carbon steel
Oxy-fuel-cut thick plate
Thick thermal-cut steel parts
Structural and welded components
Parts requiring coating or welding preparation
Suitable Materials
Carbon steel
Stainless steel
Aluminum
Galvanized steel
Copper alloys

Parameters

ConfigurationsBB / HB / HBB
Working widths800mm, 1000mm, 1300mm & 1600mm
Main processHeavy slag removal, dross removal and abrasive finishing
Typical partsPlasma-cut, oxy-fuel-cut and thick thermal-cut steel parts
Trust pointsCE Certified · Global Service
Heavy Slag Removal Machine for Thermal Cut Steel Parts | Lasvio lasvio hbb heavy slag removal machine

Slag and dross removal configurations

Choose BB for standard dross or HB / HBB for heavy slag

The correct configuration depends on how strongly the deposit is attached, the cutting process and the result required after cleaning. Send representative parts for a process test before final selection.
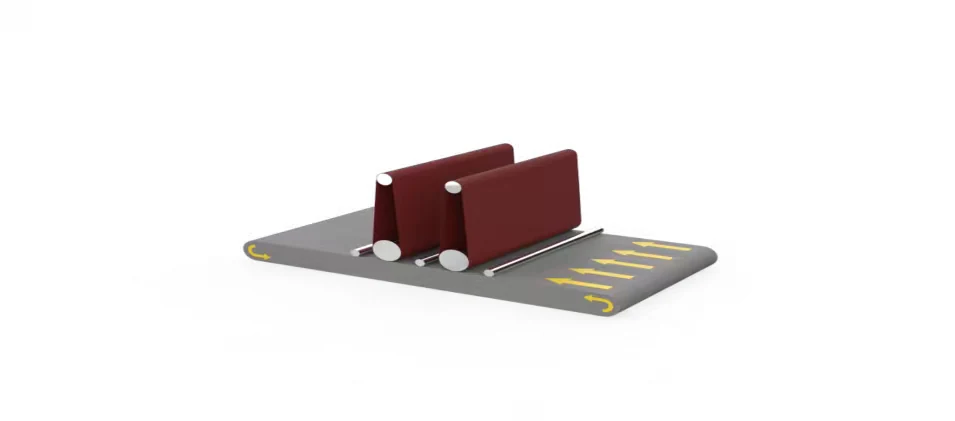
Lasvio BB slag removal configuration on white background

BB

Two abrasive belt stations

For standard laser or plasma dross and general burr removal where aggressive hammer-disc impact is not required.

  • Flexible abrasive sequence
  • Surface cleaning and burr removal
  • Working widths: 800mm, 1000mm, 1300mm & 1600mm
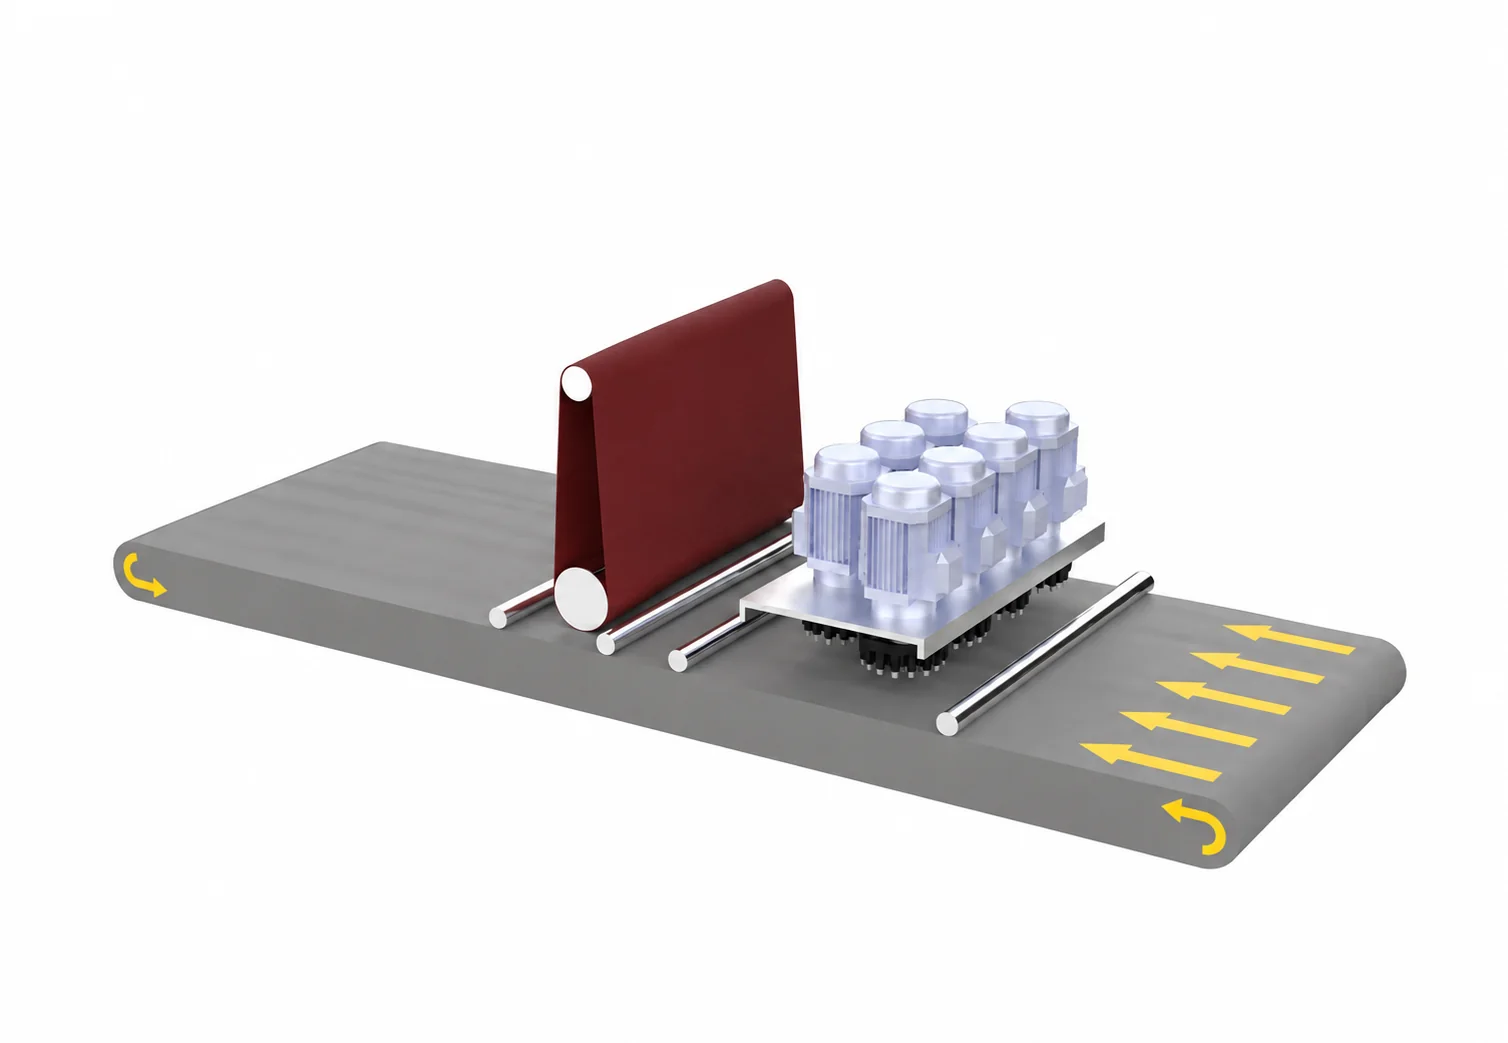
Lasvio HB heavy slag removal machine structure

HB

Hammer disc + one abrasive belt

For heavy thermal-cut slag that needs impact removal followed by one belt-cleaning stage.

  • Compact heavy-slag configuration
  • Removes strongly attached deposits
  • Working widths: 800mm, 1000mm, 1300mm & 1600mm
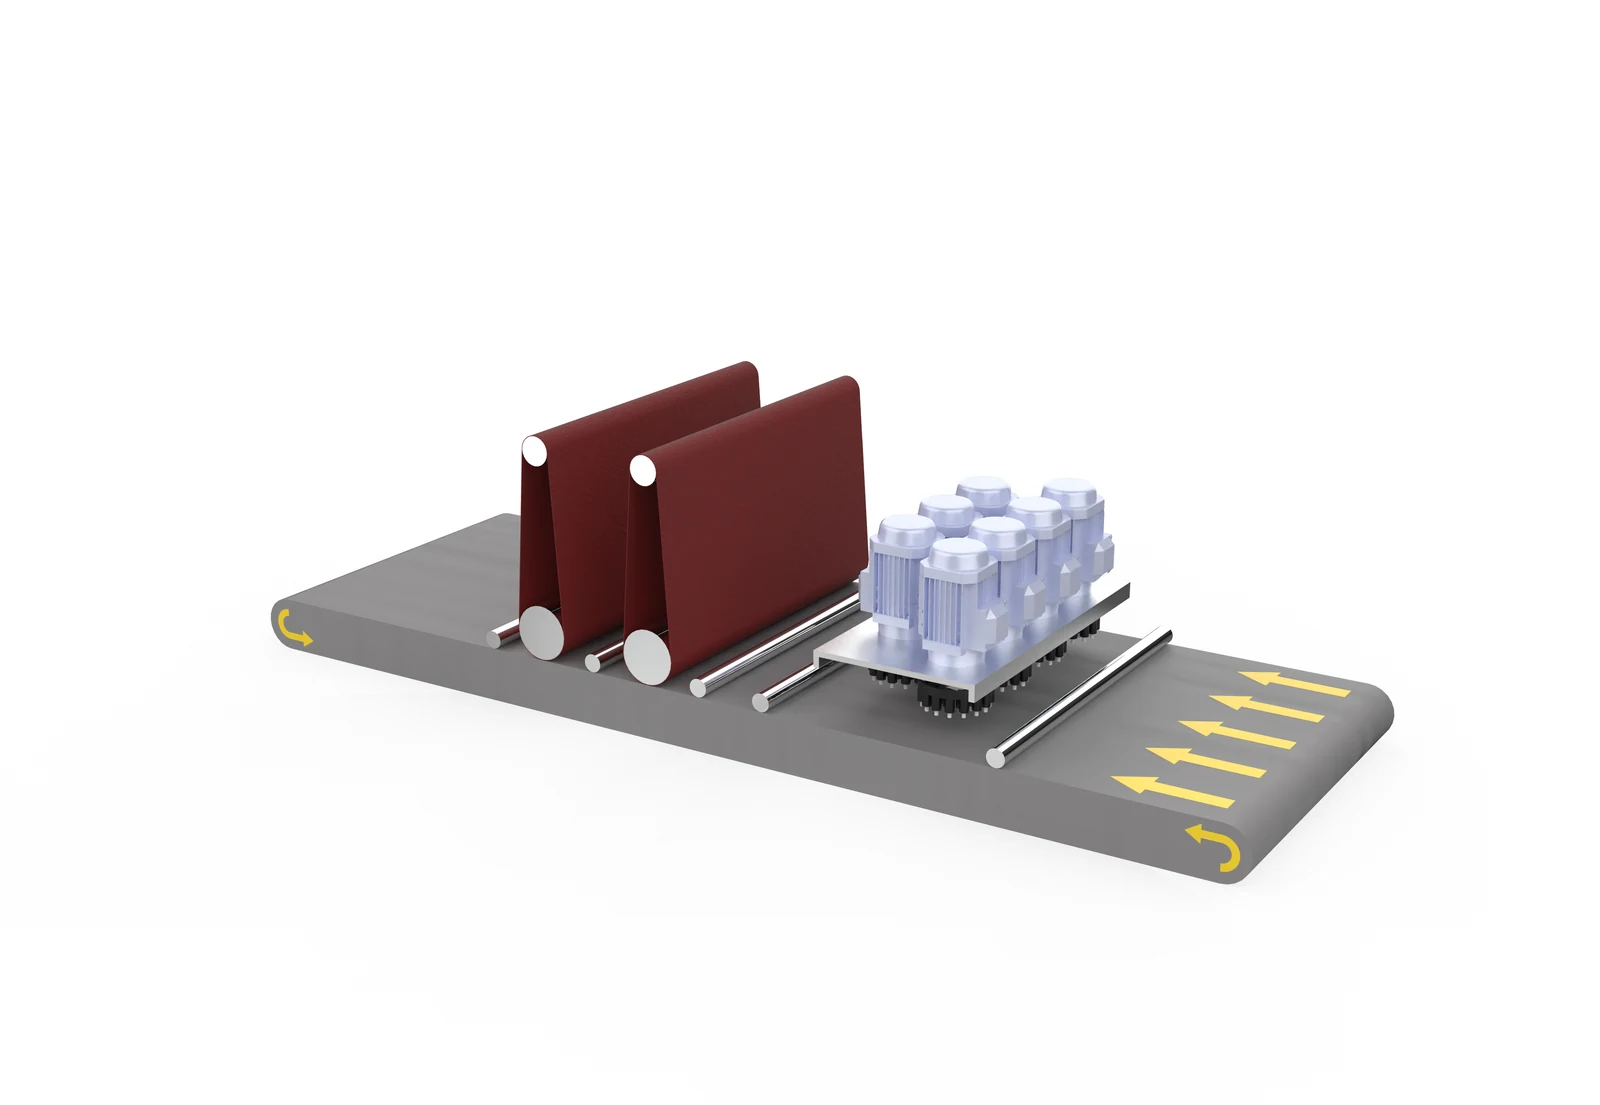
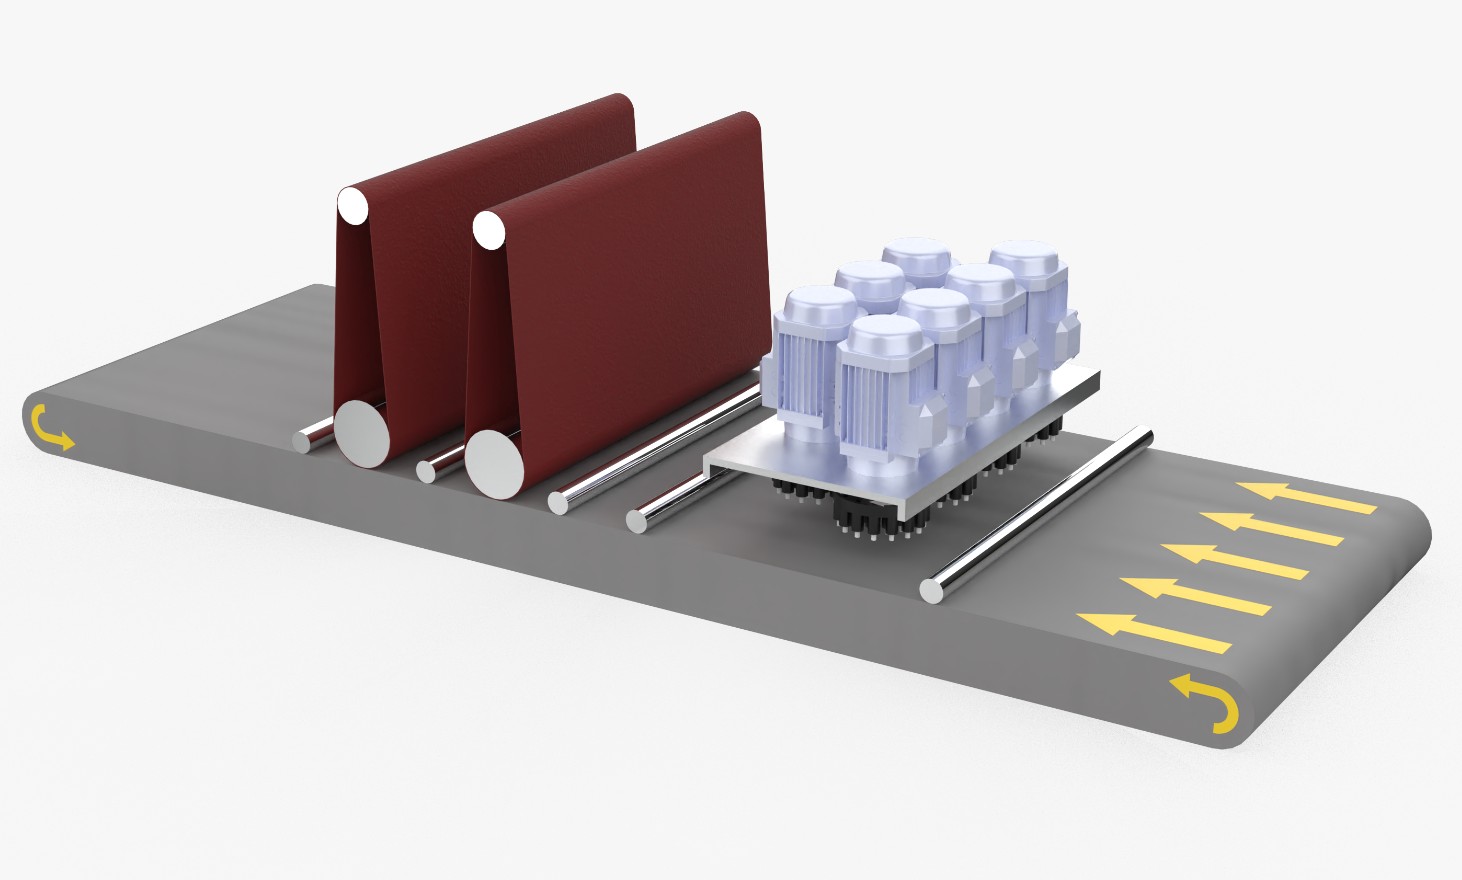
Lasvio HBB heavy slag removal configuration on white background

HBB

Hammer disc + two abrasive belts

Adds a second belt station when heavy-slag removal also requires more cleaning capacity or surface refinement.

  • More flexible post-hammer finishing
  • Suited to demanding batch production
  • Working widths: 800mm, 1000mm, 1300mm & 1600mm
Custom HBR: a hammer-disc, abrasive-belt and rotary-brush configuration can be engineered when heavy-slag removal must be followed by edge rounding. Aluminum processing requires a suitable wet dust collection system.
Machine Features

Lasvio HBB hammer-disc module for heavy slag removal

HBB Structure

H-module hammer discs fracture strongly attached plasma and oxy-fuel slag before abrasive-belt finishing. No separate pre-chipping process is required for many heavy slag applications.

Rigid Industrial Machine Structure

Heavy-duty mortise-and-tenon frame construction helps reduce vibration and supports stable processing during continuous production.
Heavy-duty frame of a Lasvio slag removal machine
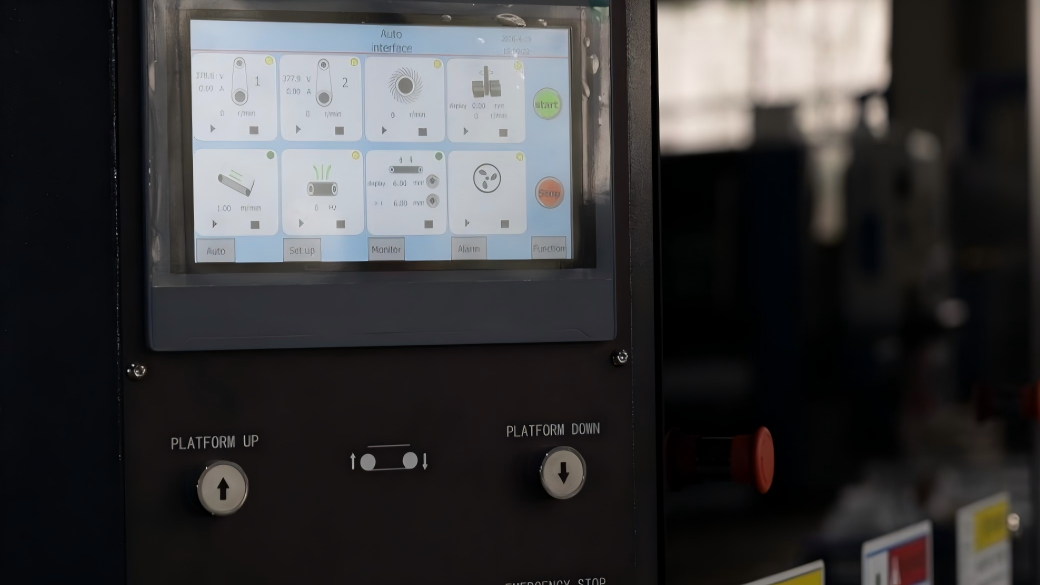
Closed-loop servo control system on a Lasvio deburring machine

Closed-Loop Servo Control

Closed-loop servo control supports repeatable positioning and consistent machine settings between production runs.

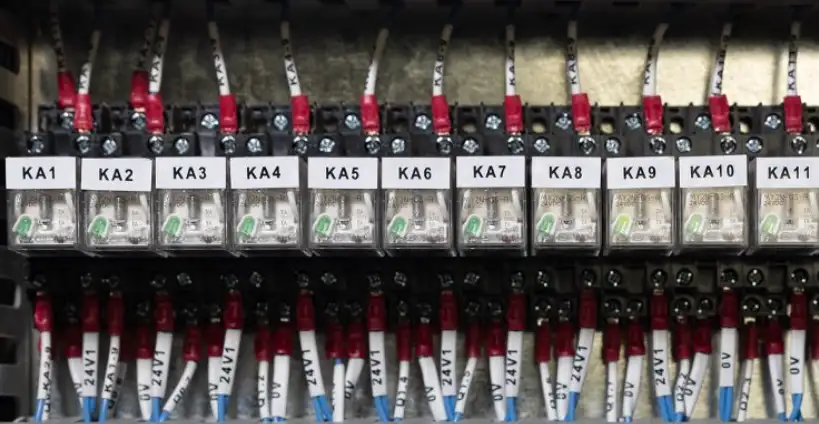
Industrial Electrical System

Labeled wiring and matching electrical documentation support maintenance, component identification and troubleshooting.
Lasvio machine electrical cabinet with labeled wiring
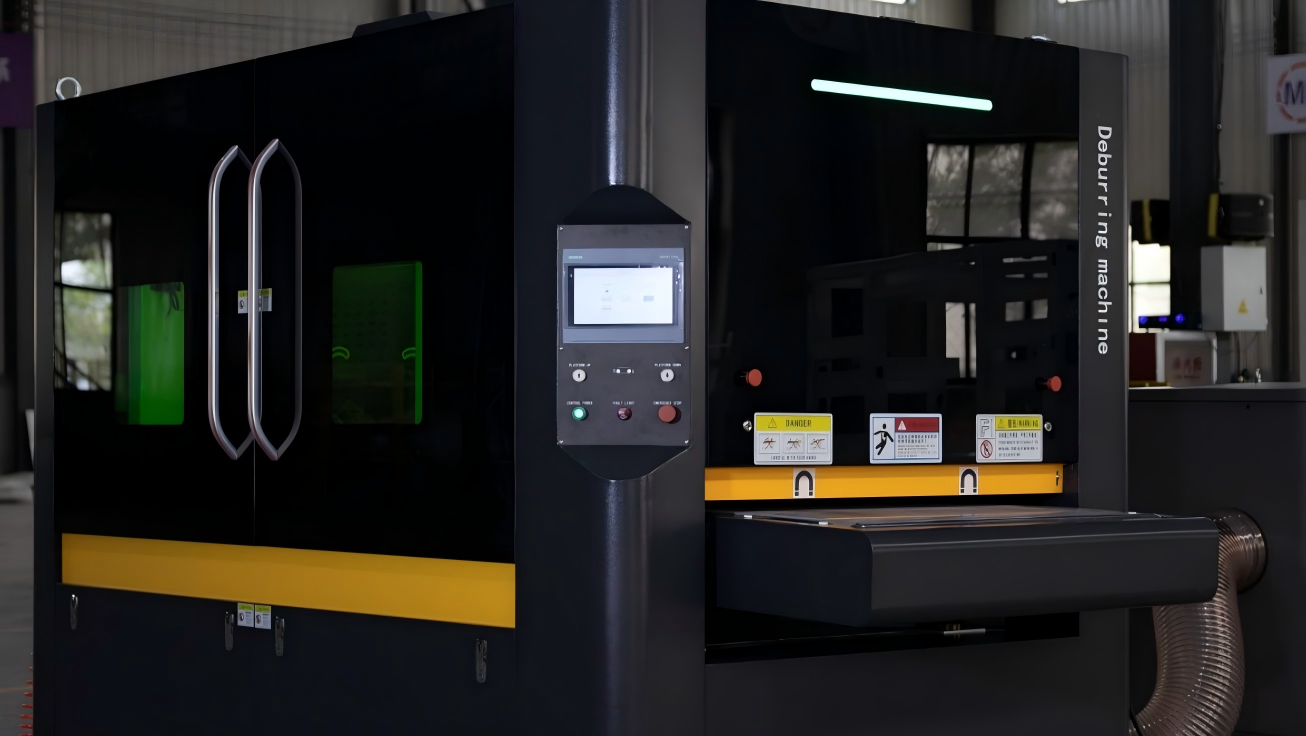
Safety enclosure and emergency stop on a Lasvio machine

Integrated Safety Protection

Enclosed processing, emergency stops and safety interlocks support operator protection during daily operation.

Processing Capability

Designed for plasma-cut, oxy-fuel-cut, and thick thermal-cut parts where slag is strongly attached and manual removal becomes a bottleneck.
Processing Functions
Heavy slag removal
Dross removal
Burr removal
Surface preparation
Production Advantages
Reduced heavy slag buildup
Cleaner edge condition
Improved welding preparation
More consistent coating preparation
Less dependence on manual grinding

Processing Flow: Applications

Welding Preparation

Remove attached cutting slag before welding to reduce manual cleanup and prepare cleaner contact edges. Select BB, HB or HBB according to deposit severity.
Weld spatter and overflow bead removal before coating

Thermal Cut Steel Parts

Process plasma-cut, oxy-fuel-cut and thick laser-cut steel parts with tooling selected for the attached slag and required finish.
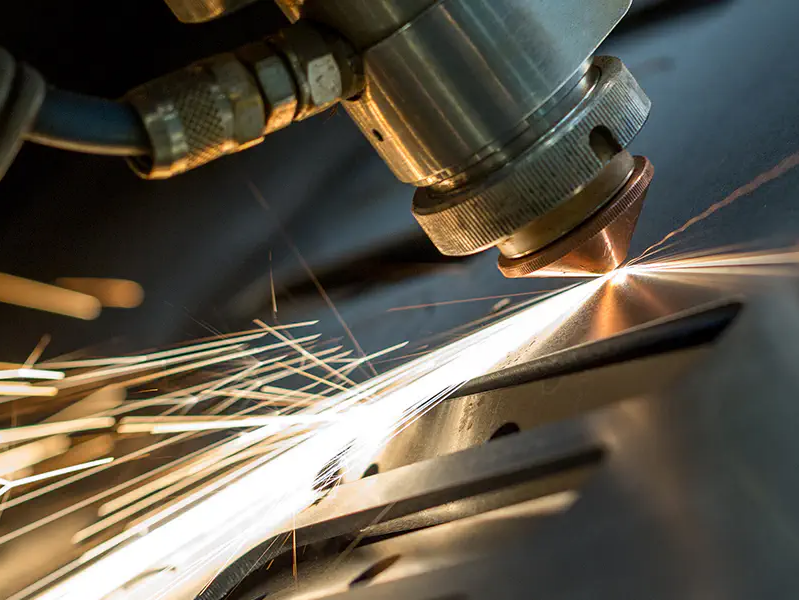
laser cutting

Metal Fabrication

Handles burrs from stamping and shearing on medium-to-large panels. Delivers a fast, consistent finish ready for powder coating or plating.

metal & fabrication

Before & After Processing

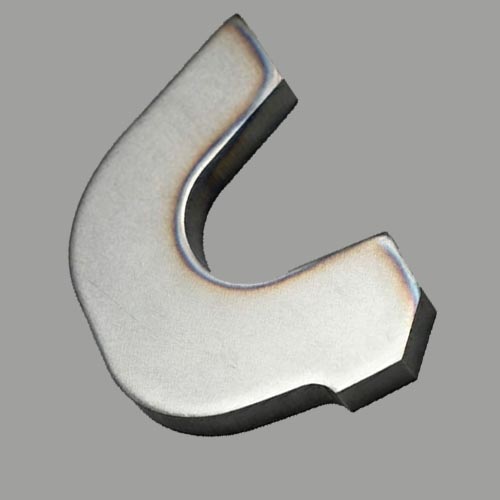
Carbon steel part after deburring and edge roundingedge rounding
After processing, metal parts achieve:

Cleaner Edges. Reduced Secondary Grinding.

  • Reduced heavy slag buildup
  • Cleaner edge condition (Optional)
  • Improved welding preparation
  • More consistent coating preparation
  • Better overall finishing appearance

FAQ

Slag or dross is resolidified material left by thermal cutting. Heavy slag is more strongly attached and may require hammer-disc impact before abrasive finishing.

Choose HB or HBB when heavy thermal-cut slag is the main problem. BB is better suited to standard dross, burr removal and abrasive finishing tasks.

Yes. Removing hard deposits and oxide buildup creates cleaner edges before welding, coating or downstream fabrication.

Send representative parts with material, thickness, cutting method and photos of the slag condition. A sample test is the safest way to confirm the configuration.

Inquiry Section

Not Sure Which Configuration Fits Your Process?

Tell us your workpiece type, production volume, and finish requirements. Our technical team will recommend the right model and module setup — and arrange a sample test on your actual parts.

Blank Form (#3)
Scroll to Top

Send An Inquiry

Blank Form (#3)